Engineered Food Storage Racking Systems
Certified heavy-duty, medium-duty, drive-in, and automated flow racking solutions specifically tailored for low-temperature food processing, cold storage warehouses, and FMCG distribution centers.
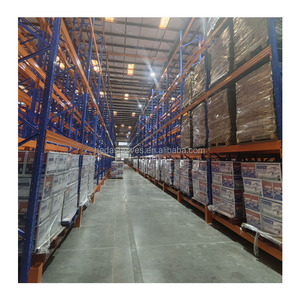 100% Selectivity
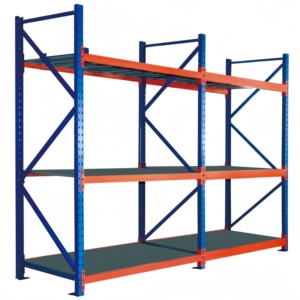 Hand-Loaded Bulk
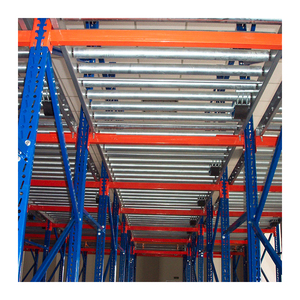 Automatic FIFO
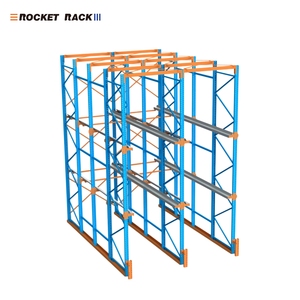 High-Density LIFO
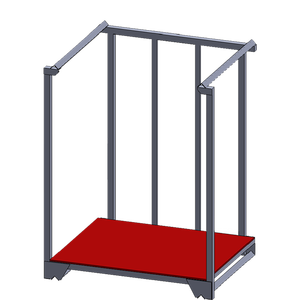 Modular Nestainer
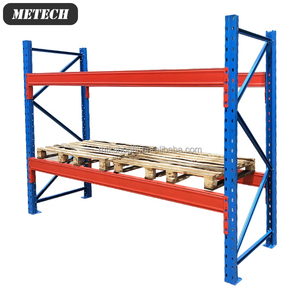 Teardrop Compatible
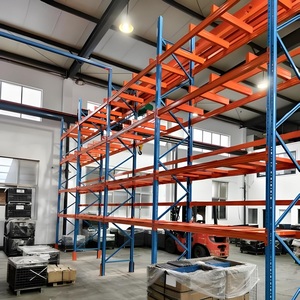 Extra Load Capacity
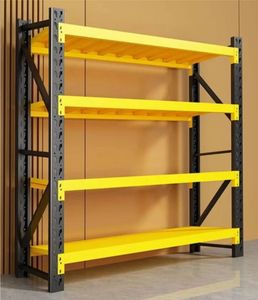 500kg/Layer Steel
1. Architectural Integrity & CE Standard EN 15512 in Food Storage Engineering
Modern food and beverage supply chains operate under relentless throughput demands, strict hygiene regulations (HACCP / FSMA), and harsh environmental conditions—ranging from high-humidity ambient packing halls to sub-zero freezer facilities operating down to -30°C (-22°F). Selecting an industrial food storage pallet racking manufacturer requires deep verification of structural compliance, metallurgical performance under thermal stress, and hygienic surface engineering.
Our CE-certified pallet racking systems strictly adhere to European standard EN 15512:2019 (Steel static storage systems - Adjustable pallet racking systems - Principles for structural design) and EN 15635 (Steel static storage systems - Application and maintenance of storage equipment). Unlike non-certified storage racks that utilize standard low-yield steel without structural calculations, our structural components undergo rigorous finite element analysis (FEA) and physical limit-state load testing to withstand both static pallet weight and dynamic forklift impact forces.
E-E-A-T Technical Insight: Cold Chain Embrittlement & Steel Grade Selection
In sub-zero cold storage facilities, standard commercial grade carbon steels suffer from Charpy V-notch impact strength degradation, transforming from ductile to brittle state. Our engineering department specifies certified high-tensile S355JR (Q355B) structural alloy steel with tested low-temperature toughness for upright frames, ensuring structural yield reserves exceeding 1.5x working load limits under continuous freezing cycles.
Surface Sanitation & Anti-Corrosion Compliance
Food storage environments present strict sanitation requirements. Unprotected steel surfaces subject to condensation risk oxidation, micro-cracking, and chemical degradation from food acid spills or chlorine sanitizer washdowns. To eliminate biological contamination risks, our factory employs two primary coating pathways:
- Food-Grade Electrostatic Epoxy Powder Coating: Utilizing non-toxic, TGIC-free epoxy-polyester thermosetting powders cured at 200°C. This creates a dense, non-porous surface finish resistant to fungal growth, chemical cleaning agents, and impact chipping.
- Continuous Hot-Dip Galvanizing (HDG): Complying with ISO 1461 standards, delivering a zinc coating thickness of 60 to 80 microns. This creates self-healing anodic protection vital for cold store entry-zone racks exposed to constant condensation and defrosting cycles.
2. Food Storage Racking System Selection Matrix
Choosing the optimal pallet racking configuration requires matching operational SKU density, inventory rotation velocity (FIFO vs. LIFO), and building clear heights. Below is a comparative technical matrix designed by our senior storage solution architects:
| Racking System Type | Space Utilization | Inventory Rotation | Ideal Food Application | Key Engineering Feature |
|---|---|---|---|---|
| Heavy Duty Selective Rack | 50% - 60% | 100% SKU Selectivity | High-SKU distribution, grocery fulfillment centers | Adjustable 50mm/75mm beam pitch, step beams for wire decking |
| Drive-In / Drive-Through Rack | 75% - 85% | LIFO (Drive-In) / FIFO (Drive-Through) | Deep-freeze meat, seafood, ice cream, seasonal batch storage | Continuous floor-to-ceiling rails, heavy-duty upright column guards |
| Gravity Pallet Flow Rack | 80% - 90% | Strict FIFO (First In, First Out) | Perishable dairy, fresh produce, high-turnover beverages | Brake rollers, magnetic speed controllers, automatic separation safety locks |
| Movable Stacking Nestainer | Dynamic Floor Storage | Flexible Batch Access | Raw material staging, seasonal agricultural harvesting | Modular welded frame, 4-way forklift entry, nestable when empty |
| Long Span Medium-Duty Rack | 60% - 70% | Manual Cartons / Totes | Manual picking food processing rooms, bakeries | Steel panels or wire mesh shelves with food-grade sanitary drop-in fit |
3. Enterprise Manufacturing Strengths & Export Leadership
As a leading Chinese manufacturer and global exporter of industrial storage equipment, Rackzzszn (Guangzhou Maobang Storage Equipment Co., Ltd.) brings over 23 years of specialized engineering experience to international buyers across North America, Europe, South America, the Middle East, and Southeast Asia.
20,000 m² Modern Plant
Equipped with 80+ automated CNC punching, cold roll-forming lines, robotic welding stations, and automatic beam end connector assembly units.
50,000 Tons Annual Steel Processing
Direct bulk steel procurement from premier state-owned mills (BaoSteel, Shougang Group) ensuring certified chemical composition and uniform physical tolerances.
South China's Longest Powder Line
Features an advanced 5-stage chemical pre-treatment spray line and 3-color single-pass electrostatic powder coating for superior coating adhesion and durability.
From initial structural survey to container loading, our complete export quality management framework is fully audited by SGS and ISO 9001:2015 standards. Every rack component leaving our facility is bundled with heavy-duty plastic wrapping, corner protectors, and steel strapping to ensure zero transit damage during long-distance ocean freight.
4. Strategic Procurement Trends in Food Storage Racking (2025–2030)
Driven by e-commerce grocery expansion, labor cost pressures, and aggressive sustainability targets, international food storage procurement managers are re-evaluating their storage infrastructure. Key technological shifts include:
A. Integration with Automated Storage and Retrieval Systems (AS/RS) & Pallet Shuttles
Manual forklift operations in sub-zero freezers suffer from high operational costs and reduced operator shift limits. The global trend is rapidly transitioning toward Radio Shuttle Racking and fully automated AS/RS High-Bay Racking. These systems require high-precision manufacturing tolerances (upright verticality alignment within ±1.5mm per 10m height) to allow autonomous shuttle carts to travel seamlessly along galvanized guidance rails at speeds up to 1.2 m/s.
B. Sanitation Engineering & Open-Profile Hygienic Beam Designs
Food safety compliance inspectors (FDA, EFSA) are increasing scrutiny on hollow tubular structural sections where internal condensation and uncleaned food residues foster bacterial growth (e.g., Listeria monocytogenes). Future-proof food storage racks incorporate open C-channel step beams or roll-formed open profiles with continuous seamless welds, eliminating uninspectable internal voids and allowing complete 360-degree washdown access.
C. High-Density Gravity Flow Automation for Perishables
With short shelf-life items like fresh milk, ready-to-eat meals, and berries, manual stock rotation errors lead to high spoilage rates. Gravity flow pallet systems automatically enforce strict FIFO inventory management. Integrated speed controllers prevent pallet acceleration over long lanes, while automatic aisle separators ensure smooth picking without pallet line pressure.
5. Regulatory Evolution & Global Compliance Benchmark
Exporting industrial pallet racking to international markets requires full alignment with regional building codes and occupational health standards. Food storage racks must meet three primary compliance pillars:
- Structural Safety Code Compliance: European EN 15512, US RMI (Rack Manufacturers Institute) Specifications, and Australian Standard AS 4084-2012. Our engineering team provides verified 2D framing layouts, structural calculations, and beam load capacity tags for local building permit applications.
- Food Contact & Indirect Chemical Safety: Ensure that all surface coatings, oil residues, and plastic accessories are non-gassing and free of VOCs or toxic heavy metals, complying with EU Regulation (EC) No 1935/2004 for indirect food packaging zones.
- Seismic & Dynamic Load Engineering: In active seismic zones (e.g., Chile, Japan, West Coast USA), storage racks must be designed with enlarged baseplates, double-anchor bolt footings, and structural cross-bracing to absorb lateral ground acceleration without catastrophic frame collapse.
Food Storage Racking Procurement FAQ
Ready to Optimize Your Food Storage Infrastructure?
Contact our structural engineering department today for custom CAD layout designs, EN 15512 load calculations, and direct factory export pricing for your warehouse project.
Get a Quote