Enterprise Fleet & Racking Systems
Featured Warehouse Storage & Automation Products
High-performance industrial rack configurations designed, structural-stress tested, and customized for automated shuttles, high-bay storage, and dense pallet management.
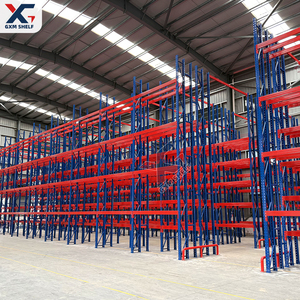
GXM Heavy-Duty Industrial Storage Rack For Pallets Durable 5-Layer Pallet Flow Rack With VNA Design Steel Warehouse Racking
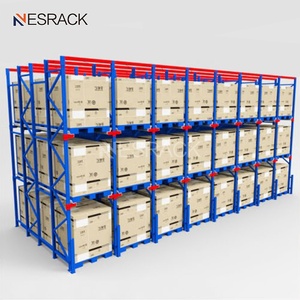
Drive-In Heavy Duty Steel Pallet Rack with 2000kg Load Capacity Seismic Reinforcement for Warehouse Storage
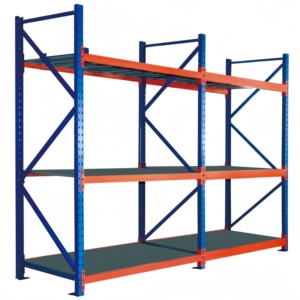
Medium Duty Long Span Metal Pallet Rack for Warehouses for Cargo & Storage Factory Price
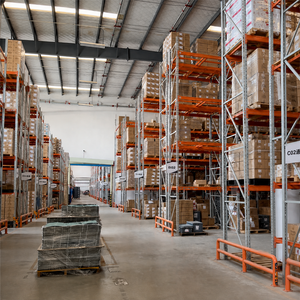
Heavy Duty Pallet Rack Back to Back Double Entry Row with Safety Guardrails for E-commerce Fulfillment Center Storage
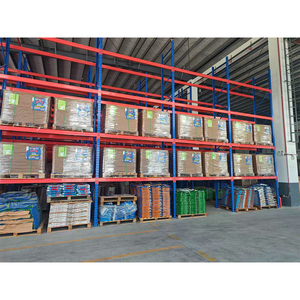
VNA Pallet Racking System Narrow Aisle High Bay Storage Solutions
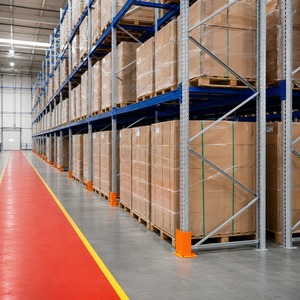
Pallet Racking System Heavy Duty Rack Industrial Pallet Storage Q235B Steel Tyre Rack Storage For Warehouses
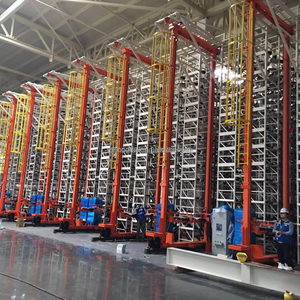
ASRS Shuttles Pallet Racking System Smart Warehouse Forklift Automation with Radio Control Cargo & Storage Equipment
Engineering Whitepaper
Architectural Superiority of CE Certified 4-Way Shuttle Systems
Modern supply chain logistics demand maximum volumetric efficiency, microsecond inventory responsiveness, and strict operational safety. The CE Certified Four Way Shuttle Racking System represents the pinnacle of automated high-density pallet storage (AS/RS).
Omnidirectional Mobility
Unlike traditional 2-way radio shuttles confined to single channels, a 4-way shuttle executes horizontal and vertical aisle switching autonomously across specially engineered precision steel tracks.
CE Compliance & Safety
Built in alignment with European Machinery Directive 2006/42/EC and EN 15095 standards. Integrated photo-electric sensors, emergency bumpers, and laser distance measurement guarantee accident-free human-machine co-existence.
90% Space Utilization
Eliminates forklift operational aisles entirely within the main rack block, elevating warehouse floor space utilization to over 90% and doubling overall pallet storage capacity compared to selective pallet rack layouts.
90%+
Space Efficiency
23+
Years Engineering Expertise
50,000t
Annual Steel Output
60+
Export Destinations
Information Gain & Systems Analysis
How Four-Way Shuttles Outperform Traditional Storage Racks
When evaluating capital expenditure (CapEx) against return on investment (ROI), supply chain directors must examine how structural racking integration interacts with automated fleet software (WCS/WMS).
| Storage Metrics | 4-Way Shuttle AS/RS | 2-Way Radio Shuttle | VNA Narrow Aisle | Selective Pallet Rack |
|---|---|---|---|---|
| Volumetric Density | Ultra High (90%+) | High (75-80%) | Moderate (60-65%) | Low (40-45%) |
| Throughput Capacity | Dynamic Multi-Vehicle Fleet | Single-Lane Dependent | Forklift Operator Bound | Forklift Operator Bound |
| Operating Height | Up to 25 Meters | Up to 12 Meters | Up to 15 Meters | Up to 10 Meters |
| Cold Chain Compatibility | Extensive (-30°C to +45°C) | Moderate (-20°C) | Restricted by Driver | Standard |
| CE Safety Certification | Full EN 15095 / EN 15635 | Basic ISO Compliance | Manual Machine Specs | Basic Static Racking Specs |
| Direct Pallet Selectivity | 100% via Fleet Routing | LIFO / Limited FIFO | 100% Direct Access | 100% Direct Access |
Mechanical and Structural Precision Engineering
A premier CE Certified Four-Way Shuttle system is not merely a steel rack; it is an ultra-precise structural machine. Uprights manufactured from high-tensile Q235B or Q355B structural steel undergo continuous cold-roll forming to guarantee deflection tolerances tighter than 1/1000th of the span length under maximum payload.
Custom multi-directional guide rails feature double-sided cold galvanization or tough powder coating applied via South China's longest continuous spray line. This delivers low rolling friction for shuttle wheels, reduced wear on LiFePO4 batteries, and decades of corrosion-free performance in high-humidity or sub-zero freezing environments.
Market Outlook 2025–2030
Future Procurement & Technology Trends in Shuttle Racking
Global logistics networks are transitioning toward hyper-automation. Procurement managers must plan racking purchases based on upcoming technological shifts.
1. Modular AI Fleet Scheduling & WCS Integration
Procurement is shifting away from fixed, single-shuttle systems toward modular vehicle fleets managed by artificial intelligence. Modern Warehouse Control Systems (WCS) dynamically calculate path planning for 20+ four-way shuttles operating simultaneously within one rack block, preventing bottlenecks during peak fulfillment shifts.
2. ESG Driven Ultra-Low Cold Chain Energy Design
With electricity prices rising, cold storage facilities are adopting 4-way shuttles because compact, high-density layouts reduce the refrigerated air volume per pallet position by up to 40%. Next-generation shuttles feature regenerative braking and rapid super-capacitor charging, reducing carbon footprints.
3. Hybrid Vertical Lifter Integration
Future procurement plans prioritize seamless synergy between four-way horizontal shuttles and heavy-duty vertical reciprocating conveyors (VRCs). This allows shuttles to switch levels effortlessly, creating true 3D spatial freedom without requiring dedicated lifters at every aisle level.
4. Standardization Under International CE Norms
Global buyers are increasingly excluding suppliers who lack certified conformity. Full certification under EN 15095 (power-driven mobile storage), FEM 10.2.02 (racking design), and EN 15635 (structural inspection) is now a mandatory prerequisite for North American and European logistics projects.
Enterprise Strength & E-E-A-T Authority
Why Global Supply Chains Partner with Rackzzszn
Rackzzszn Storage Equipment Co., Ltd. brings over 23 years of specialized manufacturing experience, structural design rigor, and global export capability to complex storage projects.
20,000 m² Modern Plant
Equipped with over 80 automated production machines including CNC punching, cold roll-forming mills, automated robotic welding stations, and precision bending lines capable of processing over 50,000 tons of structural steel annually.
Longest Spray Line in South China
Our state-of-the-art continuous powder coating line allows multi-color coating in a single pass, ensuring exceptional surface adhesion, impact resistance, and uniform paint thickness across all beams and upright frames.
SGS Verified Export Capability
With over 1,000 export containers shipped each year to 60+ countries, our packaging and container loading protocols prevent transit damage, guaranteeing smooth customs clearance and easy on-site installation.
End-to-End Project Engineering Methodology
01
Site Survey & 3D BIM Layout
Detailed millimeter-accurate space measurement, column grid calculation, and fire clearance check.
02
FEM Structural Simulation
Stress, deflection, and seismic load testing performed by certified structural racking engineers.
03
Precision Manufacturing
High-grade steel processing, continuous roll forming, automated welding, and powder coating.
04
Commissioning & Support
Export packing, on-site assembly guidance, shuttle fleet integration, and safety inspection manuals.
Procurement Knowledge Base
Frequently Asked Questions by Industrial Buyers
Essential technical guidance compiled by our senior structural engineers to assist purchasing teams and warehouse managers during system evaluation.
Why is CE Certification critical for Four-Way Shuttle Racking Systems?
CE Certification ensures compliance with strict European Health, Safety, and Environmental protection standards—specifically Machinery Directive 2006/42/EC, Low Voltage Directive 2014/35/EU, and EN 15095 (power-operated mobile storage). Without valid CE verification, automated shuttles operating in proximity to human staff pose legal compliance risks, insurance liabilities, and operational hazards in international jurisdictions.
What concrete floor specifications are required for 4-way shuttle rack installation?
Because automated four-way shuttles move at high speeds (up to 1.5–2.0 m/s) and carry payloads up to 1,500 kg per pallet, floor flatness is paramount. The concrete slab should comply with EN 15620 (Class 300 or better) or FM2 special standards. Floor load capacity must support point loads from high-bay upright footplates, typically ranging from 5 to 15 tons per post depending on height.
How do 4-way shuttle systems handle low-temperature cold storage environments?
For sub-zero applications down to -30°C, our system utilizes special cold-temperature structural steel grades with enhanced impact resistance to prevent cold brittleness. Electrical components, lithium iron phosphate (LiFePO4) battery packs, internal optical sensors, and lubricants are specifically rated for low-temperature operation, featuring automatic internal heating circuits to avoid condensation issues during level switches.
What is the typical Return on Investment (ROI) timeline for an automated 4-way shuttle system?
While initial capital investment for shuttle automation is higher than static racking, ROI is typically achieved within 18 to 36 months. Financial savings stem from a 50% reduction in warehouse footprint requirements, lower land acquisition or leasing costs, minimal forklift usage, reduced labor overhead, lower heating/cooling energy expenses, and reduced pallet handling damage.
Can Rackzzszn supply custom rack colors, dimensions, and OEM branding for large projects?
Yes. As a direct manufacturer with in-house design engineering, roll-forming lines, and South China's longest powder coating spray line, we fully customize frame heights, depth channels, beam section profiles, and RAL powder coat colors to meet your corporate design identity or structural requirements.
Optimize Your Warehouse Capacity with Certified 4-Way Shuttle Systems
Work directly with our senior structural engineers to design a custom high-density automated racking system tailored to your ceiling height, load specifications, and operational throughput targets.