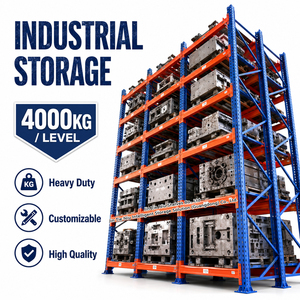
Engineered Product Lineup
High-Performance Industrial Racking & Automated Logistics Systems
Explore certified storage systems custom manufactured to optimize floor footprint, increase cube utilization by up to 85%, and seamlessly interface with VNA turret trucks, AGVs, and Automated Guided Systems.
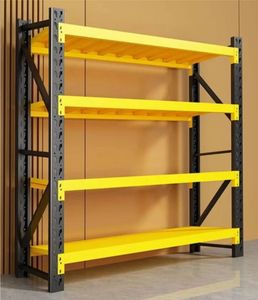
Custom Adjustable Medium-duty Load-Bearing 500kg/Layer Steel Racks Warehouse Industrial Stack Storage Racking Shelving System
Contact Us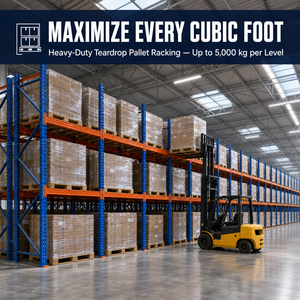
Large Scale E-Commerce Logistics Warehouse Pallet Racking System Customized High Load Industrial Conventional Heavy Duty Rack
Contact Us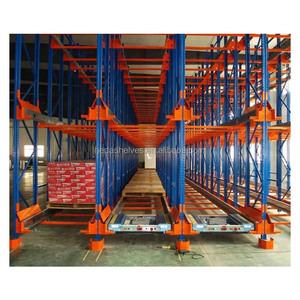
Auto Shuttle Racking System Innovative Pallet Racking Intensive Shuttle Racks Intelligent Cold Storage Shuttle Rack Automatic
Contact Us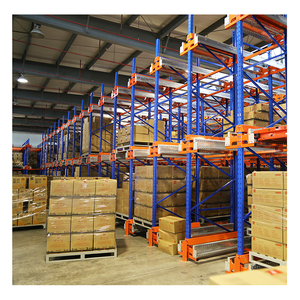
Customizable Heavy Duty Steel Pallet Shuttle Rack for Warehouse Storage Cargo & Storage Equipment OEM/ODM
Contact Us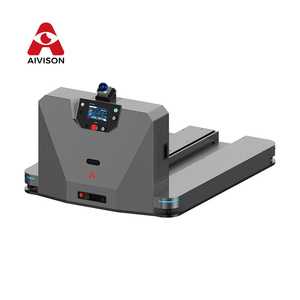
China AGV Manufacturer Automated AMR Open Pallet / Closed Pallet Handling Robot For Warehouse Logistics
Contact Us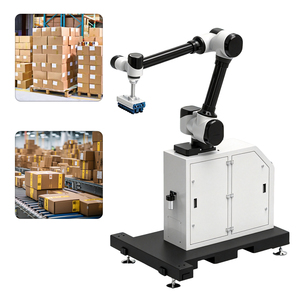
WP-50 Smart Automatic Carton Case Handling Packaging System Reach 1780mm High Speed Electric Pallet Stacking Robotic Palletizer
Contact Us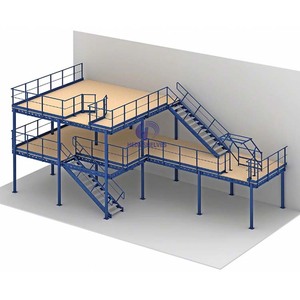
High Q235 Steel Warehouse Multi-level Mezzanine Flooring Rack Industrial Storage Platforms Shelving
Contact UsStructural Engineering Standard of CE Certified Very Narrow Aisle (VNA) Racking
In modern industrial logistics, floor footprint efficiency is directly tied to operational profitability. Very Narrow Aisle (VNA) Pallet Racking systems represent the pinnacle of static high-density storage design. By compressing operating aisle widths from standard selective dimensions (typically 3.5 to 4.2 meters) down to 1.5 to 1.8 meters, VNA configurations instantly reclaim up to 45% of lost floor space while preserving 100% direct SKU accessibility.
However, achieving structural stability at heights scaling up to 18 meters requires strict compliance with international manufacturing and design mandates. As a premier CE Certified Narrow Aisle Pallet Racking Manufacturer, Rackzzszn Storage Equipment Co., Ltd. builds racking arrays strictly conforming to EN 15512 (Structural steel racking systems - Adjustable pallet racking systems - Principles for structural design), EN 15620 (Tolerances, deformations and clearances), and FEM 10.2.02 guidelines.
Engineering Fact: At storage heights exceeding 12 meters, dynamic frame deflection and slab vertical displacement become critical risk factors. Our engineering team calculates beam flexure under maximum safe working load (SWL) to ensure deformation does not exceed L/200, protecting narrow-aisle VNA turret trucks from structural collision.
Every structural upright profile produced in our 20,000 m² facility is cold-roll formed from certified high-tensile steel grades (Q235B and Q355B). The mechanical design features continuous teardrop or diamond punching pattern matrixes, enabling 50mm or 75mm pitch level adjustability. This rigidity guarantees that dynamic braking loads from VNA articulated fork trucks or wire-guided stacker cranes are fully absorbed and safely transferred into the reinforced concrete floor slab.
Factory Advantage
Why Tier-1 Global Logistics Providers Source from Rackzzszn
Direct integration of raw material procurement, structural engineering, precision roll-forming, automated electrostatic powder coating, and global deployment services.
South China's Longest Spray Line
We operate the longest continuous automated powder-coating line in South China. Featuring multi-stage pre-treatment wash chambers and a triple-color rapid-change electrostatic booth, our coating guarantees non-porous 60-80 micron epoxy-polyester surface protection resisting corrosion, chemical spills, and abrasive industrial wear.
End-to-End Layout Engineering
Second-hand drawings often hide critical structural discrepancies. Our project team conducts initial laser floor level analysis, column-grid mapping, and clearance calculations. We generate full 2D AutoCAD execution prints and 3D BIM models detailing fire sprinkler clearances and VNA guide rail specs before manufacturing begins.
Traceable Structural Auditing
Every shipment undergoes rigorous Quality Assurance. We verify steel coil mill certificates, perform destructive tensile strain tests on weld joints, and measure structural deflection tolerances. Our CE certification guarantees total compliance for European Union imports and high-seismic zone installations.
Future Procurement Trends in High-Density Narrow Aisle Racking Systems
The global warehousing landscape is undergoing a systemic transition driven by land scarcity, urban micro-fulfillment requirements, and rapid integration of robotic automation. Procurement officers and supply chain executives must plan racking infrastructure not just for present pallet dimensions, but for long-term scalability and technological adaptability.
1. Convergence of VNA Racking with Autonomous Mobile Robots (AMRs) & AGVs
Traditional VNA layouts rely heavily on human-operated man-up or man-down turret trucks guided by mechanical steel angles or inductive floor wire signals. However, next-generation procurement cycles focus on Hybrid VNA-AMR Integration. Open-bottom and closed-bottom pallet handling robots (such as autonomous reach trucks and AMR stackers) require exact dimensional tolerances, specialized floor-level guide channels, and high-contrast optical positioning targets installed directly on rack upright faceplates.
2. High-Density Radio Shuttle & ASRS Automation Synergies
While standard VNA provides 100% individual pallet access, high-volume fast-moving consumer goods (FMCG) and cold storage facilities are increasingly specifying VNA Deep-Lane Radio Shuttle Racks. By combining narrow operating access channels with automated self-powered shuttles running along interior racking channels, warehouses achieve volumetric storage utilization rates above 85% without increasing operating footprint.
3. Cold Chain Thermal-Resilient Steel Metallurgy
Sub-zero logistics facilities (-25°C to -30°C) experience thermal contraction and material embrittlement in standard carbon steel profiles. Modern procurement standards mandate certified Q355B cold-formed structural steel treated with low-temperature ductile impact resistance, preventing micro-fractures under high-load dynamic impacts from forklift tines.
High-Density Industrial Storage Matrix: System Comparison
| Racking Architecture Type | Required Aisle Width | Storage Density Index | SKU Selectivity Ratio | Forklift Equipment Compatibility | Capital Investment (CAPEX) |
|---|---|---|---|---|---|
| Selective Pallet Racking | 3.5m – 4.2m | Standard (40-50%) | 100% Direct Access | Standard Counterbalance / Reach Truck | Low Base Cost |
| Very Narrow Aisle (VNA) | 1.5m – 1.8m | High (75-85%) | 100% Direct Access | VNA Articulated Truck / Wire-Guided Turret | Moderate – High Efficiency |
| Double-Deep Pallet Rack | 3.0m – 3.3m | Medium-High (60-65%) | 50% Immediate Access | Deep-Reach Pantograph Truck | Moderate |
| Automated Radio Shuttle | 1.6m – 2.0m | Maximum (85-90%) | LIFO or FIFO Bulk Channel | Standard Forklift + Automated Shuttle Robot | Higher Initial / Fast ROI |
| ASRS Stacker Crane System | 1.4m – 1.6m | Ultra (90%+) | 100% Automated Access | Fully Automated High-Bay Crane Rail | Enterprise Automated CAPEX |
Industrial Engineering & Plant Infrastructure: Rackzzszn Capability Overview
Rackzzszn Storage Equipment Co., Ltd. (founded in 2001) has established itself over 23 years as a foundational manufacturing hub for international supply chain infrastructure. Operating out of Guangzhou, China, our modern 20,000 square meter industrial park integrates heavy-duty raw material processing, automated continuous roll-forming lines, precision robotic welding stations, and specialized packaging systems built for long-distance container ocean freight.
In-House Tooling & Metallurgical Testing
Quality begins with raw material integrity. We source premium-grade structural coil steel strictly compliant with GB/T 709 and EN 10025 standards. Our in-house metallurgical laboratory verifies yield strength, ultimate tensile strength, and percentage elongation after fracture. By maintaining total control over upright profile section modulus calculations and beam connector hook engagement geometry, we guarantee zero failure rates under rated load capacities.
Global Export Logistics & On-Site Installation Support
Delivering over 1,000 export containers annually to 60+ countries requires meticulous logistics engineering. Uprights and beams are bundled using high-tensile steel banding, protective corner guards, and moisture-barrier shrink films to eliminate transit damage. Furthermore, every project package includes detailed 3D exploded structural assembly guides, component marking schedules, and remote/on-site engineering installation oversight.
Procurement Guidance
Frequently Asked Questions on CE Certified VNA Systems
Technical answers prepared by our structural design engineers to guide your warehouse planning, slab compliance, and procurement decisions.
What concrete floor slab specifications are required for VNA racking installations?
VNA racking systems impose high point loads through upright baseplates due to their elevated heights (up to 18m). Slab construction must strictly comply with DIN 18202 or TR34 (Free Movement & Defined Movement categories). For high-bay VNA operated by wire-guided turret trucks, floor levelness tolerances typically require Superflat (SF) or Category 1 classification. Slab depth should generally be a minimum of 200mm to 250mm of reinforced concrete with minimum compressive strength of C30/37.
What guidance systems are available for Very Narrow Aisle (VNA) forklifts?
We supply two primary VNA guide options: 1. Mechanical Guide Rails: Heavy-duty structural steel angle profiles (e.g., L75x75x6 or L100x75x8) floor-anchored alongside the full length of the rack aisle to physically guide truck side-wheels. 2. Inductive Wire Guidance: A frequency-emitting wire embedded into a 15mm-deep floor saw-cut along the aisle center, allowing unhindered pallet picking at ground level without physical steel rail barriers.
How does CE Certification impact international compliance and safety audits?
CE Certification confirms that our structural steel racking complies fully with European Union health, safety, and environmental protection legislation. Specifically, it validates that structural calculation models adhere to EN 15512 and FEM 10.2.02 standards. This certification streamlines local building permit approvals, satisfies corporate insurance risk audits, and verifies load capacity markings (Safety Load Notices) installed on rack frames.
Can Rackzzszn VNA systems be customized for cold storage and freezer applications?
Yes. For cold storage (-25°C to -30°C), we utilize certified cold-resilient steel grades (such as Q355B with low-temperature impact testing) and specially formulated epoxy-polyester powder coatings or hot-dip galvanized surface finishes. Our engineering team also factors thermal shrinkage into structural beam connector tolerances to prevent binding or joint fatigue during temperature fluctuations.
What is the standard manufacturing lead time for full container export orders?
Standard production lead time for standard project arrays (1 to 5 40ft High Cube containers) is 15 to 20 business days following 2D layout sign-off and engineering approval. Thanks to South China’s longest automated continuous powder coating line and high-speed multi-station roll-forming lines, we maintain industry-leading production speed without sacrificing quality control testing.
Do you provide customized structural calculations and seismic design packages?
Yes. Our structural engineering group provides project-specific engineering reports including finite element analysis (FEA), load distribution diagrams, frame bracing specs, and seismic baseplate anchor sizing tailored to local building code requirements (including US RMI standards, Eurocodes, and AS4084 guidelines for high-seismic zones).
Global Engineering Support
Transform Your Warehouse Volume with CE Certified Precision VNA Racking
Send your floor plan, clear ceiling height, and pallet load specs. Our experienced storage engineers will deliver a customized 2D/3D layout design and transparent factory-direct pricing quote within 24 hours.