High-Performance Storage Equipment & Systems
Explore our core engineering product line. Manufactured to international standards for distribution centers, pharmaceutical storage, cold chains, and heavy manufacturing.
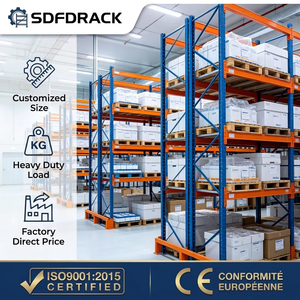
Heavy Duty Pharmaceutical Selective Pallet Racking
Adjustable high-load steel racking optimized for medical warehouses and drug distribution centers requiring GMP compliance and 100% SKU selectivity.
Contact Us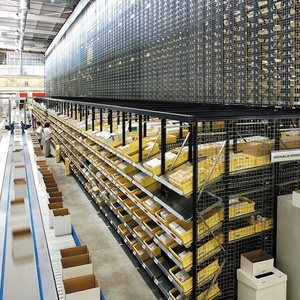
High Efficiency 5-Layer Carton Gravity Flow Rack
CE-certified smooth gravity flow system for high-turnover fulfillment centers, providing automatic FIFO stock rotation and reduced picking labor.
Contact Us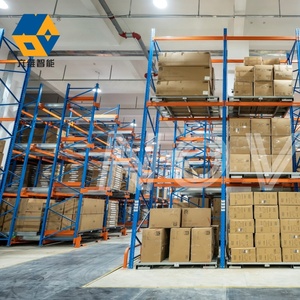
Semi-Automatic 2-Way Radio Shuttle Pallet System
Remote control radio shuttle car system designed for high-density deep-channel storage, eliminating forklift aisle movement and maximizing building utilization.
Contact Us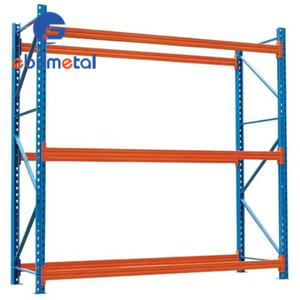
Heavy Duty Modular Shelving & Industrial Pallet Rack
Heavy structural storage racking engineered with high-yield strength steel for versatile pallet loads, bulk items, and industrial raw material storage.
Contact Us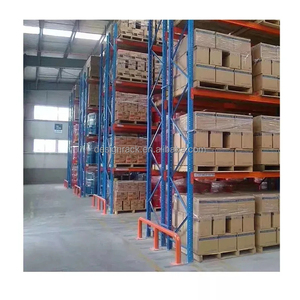
Custom Q235B Steel CE/ISO Certified Heavy Duty Racking
Precision-rolled Q235B steel racking configured to bespoke warehouse specs. Features electro-static powder coating and certified beam load capacity.
Contact Us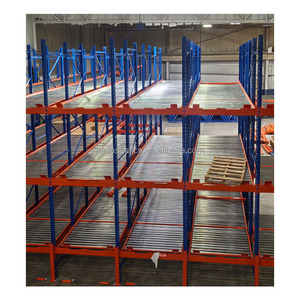
Industrial Heavy Goods Pallet Gravity Flow Racking
Dynamic roller bed pallet flow racking for high-density FIFO operations. Ideal for perishable inventory, cold stores, and fast-moving FMCG hubs.
Contact Us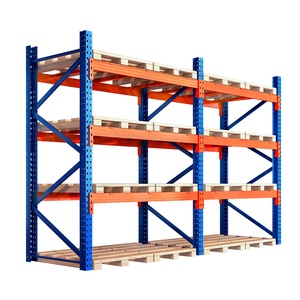
Industrial Heavy Duty Metal Stacking Rack Units
Modular steel stacking frames and post pallets designed for flexible warehouse storage, temporary volume surges, and container transport protection.
Contact Us
Large Span Custom Steel Structure Warehouse Buildings
Turnkey prefabricated metal factory buildings and industrial warehouse structures designed to integrate seamlessly with high-bay pallet racking.
Contact UsExecutive Technical Whitepaper: Evaluating Pallet Shuttle Manufacturers in China
In modern intra-logistics, spatial efficiency and throughput speeds dictate operational profitability. As global supply chains face escalating real estate costs and warehouse labor shortages, Pallet Shuttle Systems—comprising semi-automated 2-Way radio shuttles and fully automated 4-Way AS/RS shuttles—have emerged as the definitive benchmark for high-density storage capability. China has solidified its position as the world's primary manufacturing hub for these advanced storage systems, offering unparalleled structural steel quality, robotics integration, and cost efficiencies.
However, selecting the right partner among China's best pallet shuttle system manufacturers requires a comprehensive evaluation that extends beyond initial equipment purchase price. Logistics directors and warehouse engineers must audit structural steel engineering standards (FEM 10.2.02, EN 15512, RMI), battery chemistry efficiency, optical sensor reliability, Warehouse Control System (WCS) integration capabilities, and post-installation support infrastructure.
Key Takeaway for Sourcing Directors
A high-density shuttle system isn't merely steel shelving; it is an integrated mechatronic ecosystem. A 2mm tolerance deviation in deep-channel rail installation can lead to shuttle jams, sensor misalignments, and catastrophic operational downtime. OEM/ODM capability, precision manufacturing, and rigorous factory testing are essential selection criteria.
The Technical Architecture of Modern Pallet Shuttle Systems
A Pallet Shuttle System replaces conventional forklift aisles with deep-storage channels equipped with precision-engineered guide rails. Autonomous, battery-powered shuttle vehicles travel beneath the stored pallets to elevate, transport, and deposit unit loads cleanly and rapidly.
2-Way Radio Shuttle Systems
Operated via handheld RF controllers or tablet interfaces, 2-Way shuttles handle longitudinal vehicle movement along dedicated channels. Forklifts lift the shuttle car into the desired channel bay, where it independently executes LIFO (Last-In, First-Out) or FIFO (First-In, First-Out) indexing routines.
- Best Suited For: High volume per SKU, cold storage (-25°C to -30°C), beverage hubs, and buffer warehousing.
- Load Range: 500 kg to 1,500 kg per pallet unit.
- Speed Capability: Up to 1.1 m/s (unloaded) / 0.8 m/s (loaded).
4-Way Automated Guided Shuttles (4D System)
The pinnacle of high-density warehouse automation. 4-Way shuttles travel longitudinally across storage channels and laterally along cross-aisles without requiring forklift transportation. Interfaced directly with vertical elevators and WMS/WCS software, they form a fully automated matrix storage network.
- Best Suited For: E-commerce fulfillment, complex multi-SKU distribution hubs, and smart factories.
- Key Advantage: Eliminates human forklift operators entirely within high-bay storage racks.
- Scalability: Fleet size can scale dynamically as throughput demands grow.
Engineering Comparison: Selective Racks vs. Drive-In vs. Pallet Shuttle
| Storage Metric / Technology | Selective Pallet Racking | Drive-In Racking System | Semi-Automated Pallet Shuttle | 4-Way Automated AS/RS Shuttle |
|---|---|---|---|---|
| Volumetric Space Utilization | 40% – 50% | 65% – 75% | 80% – 85% | 85% – 92% |
| SKU Selectivity | 100% (Direct Access) | Very Low (LIFO) | High (per level/channel) | High (Dynamic Matrix) |
| Forklift Damage Risk | Moderate | Extremely High (Drives into rack) | Extremely Low (Stays outside) | Zero (Automated) |
| Operating Mode | Manual Forklift | Manual Forklift | Semi-Automated (Radio RF) | Fully Automated (WCS System) |
| Throughput Speed (Pallets/Hr) | 20 – 30 | 15 – 25 | 40 – 60 | 80 – 120+ |
| Cold Storage Efficiency | Low (Heated space wasted) | Moderate | Excellent (Minimal air gaps) | Superior (Unmanned dark warehouse) |
Future Procurement Trends in Pallet Shuttle Systems (2025–2030)
Global logistics managers are transitioning from static storage systems to intelligent, dynamic automation. Sourcing teams evaluating China's OEM racking market must align their specs with emerging global tech standards:
1. LiFePO4 & Supercapacitor Power
Legacy lead-acid batteries are obsolete. Modern procurement specs mandate Lithium Iron Phosphate (LiFePO4) batteries or supercapacitors featuring fast-charging capability (80% charge in 30 minutes) and operating temperatures down to -30°C without thermal decay.
2. AI-Driven Fleet Management
Advanced WCS software now incorporates predictive algorithms that analyze order flow, dynamically reorganizing pallets during off-peak hours to compress travel times and optimize picking speed for next-day shipping orders.
3. Hybrid High-Bay Structures
Integration of shuttle racks directly into building superstructures (Rack-Supported Buildings) is rapidly growing. This approach eliminates the need for separate factory wall cladding and structural columns, delivering maximum cube utilization.
Technology & Development Trends: What Distinguishes Top Chinese Manufacturers
Leading Chinese racking factories have evolved from low-cost steel fabricators into high-tech material handling equipment engineering hubs. When sourcing pallet shuttle systems from China, tier-one manufacturers set themselves apart through several key technical innovations:
High-Precision Cold-Formed Steel Profiles
Using structural steels like Q235B and high-strength Q355B, advanced factories deploy continuous multi-station cold roll-forming lines. Beam and rail profile tolerances are maintained within ±0.5mm over a 12-meter length, ensuring micro-smooth shuttle car transit and avoiding wheel vibrations.
Multi-Sensor Laser Positioning & Safety Arrays
Modern radio shuttle cars incorporate photoelectric sensors, laser distance measuring sensors, motion limit sensors, and mechanical anti-collision bumpers. This multi-layered array prevents pallet mis-positioning, detects damaged pallets instantly, and protects operators in shared aisles.
Electrostatic Powder Coating Excellence
Durability in high-humidity or cold-chain environments depends on surface finishing. Leading factories utilize automated multi-stage pre-treatment lines (degreasing, phosphating) combined with continuous powder coating ovens to deliver corrosion resistance capable of withstanding 500+ hours of salt-spray testing.
Why Partner with Rackzzszn Storage Equipment Co., Ltd.
With over 23 years of dedicated engineering and manufacturing experience, Rackzzszn Storage Equipment Co., Ltd. stands among China's premier manufacturers of heavy-duty pallet racking, cantilever systems, mezzanines, and semi-automated pallet shuttle racks. Our 20,000 m² facility delivers custom-designed storage equipment to clients across 60+ countries worldwide.
Longest Spray Line in South China
Our facility operates South China's longest automated powder coating spray line. This advanced production setup enables simultaneous 3-color coating passes, delivering rapid turnaround times, flawless coating adhesion, and superior rust protection for demanding industrial projects.
Full-Lifecycle Engineering Support
We provide comprehensive project execution: from initial site survey and 2D/3D BIM layout design to structural load calculations, custom factory fabrication, export-grade wooden pallet bundling, remote assembly guidance, and annual rack safety inspections.
Frequently Asked Procurement & Engineering Questions
Get answers to common technical, operational, and commercial questions from our senior storage engineering team.
Optimize Your Warehouse Storage Capacity Today
Connect with our senior engineering team to receive customized 2D/3D storage layout proposals, structural load calculations, and competitive OEM factory pricing within 24 hours.