Heavy-Duty Industrial Rack Systems & OEM Solutions
Explore our factory-direct precision engineered racking systems, stacker crane structural frames, and heavy-load material handling equipment manufactured for global export.
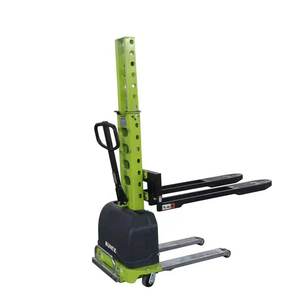
Runtx Brand Self Loading Electric Hand Pallet Stacker Self Loading with Car Lifting Stacker
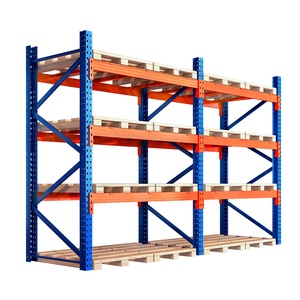
Industrial Heavy Duty Storage Shelves System Stacking Units Metal Rack Warehouse Steel Pallet Racking
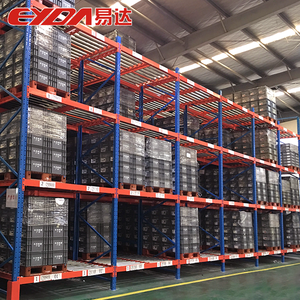
5 Layer Metal Pallet Flow Rack Gravity Storage Racks Heavy Duty Multi-Level Warehouse Industrial Cargo Storage Equipment
Heavy Duty Steel Pallet Racking System Warehouse Storage Rack With Wire Mesh Decking Factory
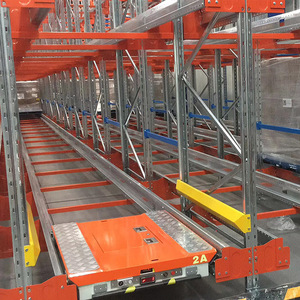
Jracking CE-Certified Radio Shuttle Rack System Space-Saving & Automated Storage Racking For Cold Storage Warehouses
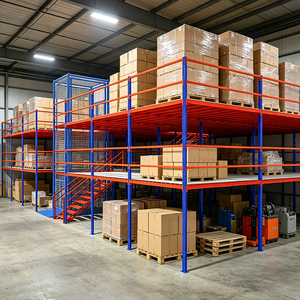
Warehouse Mezzanine Racking System Multi Level Steel Platform Shelving For Industrial Logistics Pallet Storage with Staircase
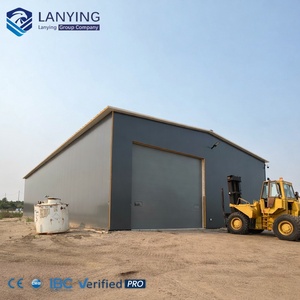
Free Design Prefabricated Steel Factory Industrial Warehouse Buildings
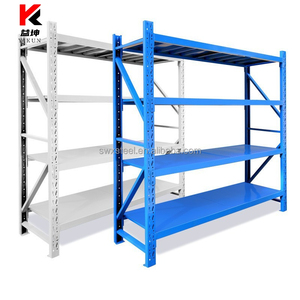
Heavy Duty Steel Adjustable Drive-In Warehouse Pallet Rack System Powder Coated Anti-Rust Finish Compact Multi-Layer LIFO
Architectural Mechanics of Crane Supported Racking Systems
Understanding the mechanical convergence of structural racking, overhead bridge crane guide runways, and automated stacker cranes (AS/RS) for ultra-high-density industrial logistics.
High Structural Load Deflection Rigidity
Calculated according to FEM 10.2.02 and EN 16681 standards. Uprights utilize high-yield strength structural steel (Q355B / Q460B) engineered to maintain horizontal deflection tolerances within L/400 to L/600 during full crane travel cycles.
Seismic & Dynamic Fatigue Resilience
Integrated with heavy diagonal truss bracing systems and dynamic energy dissipation damper brackets. Resists multi-axis dynamic vibration induced by rapid crane acceleration, emergency braking, and seismic events.
Custom OEM Bracket & Rail Geometry
Direct OEM roll-forming and laser-cut connection plates matching crane rail profiles (KBK, A-Rail, SQUARE-Rail). Provides millimeter-level alignment precision for seamless trolley travel and zero derailment risk.
When sourcing Crane Supported Pallet Racking, procurement teams must differentiate between Top-Running Overhead Bridge Crane Racking (where crane runways rest on rack column caps to handle heavy localized dies/machinery up to 10+ Tons) and AS/RS Automated Stacker Crane Racking (where floor-guided stacker cranes utilize top rack-mounted guide rails for high-speed automated pallet storage up to 45 meters in height). Custom OEM design ensures the moment frame stiffeners are optimized for the exact dynamic shear force vectors of your material handling hardware.
| Engineering Metric | Overhead Crane Rack System | AS/RS Stacker Crane System | Rack-Supported Building (RSB) |
|---|---|---|---|
| Max Storage Height | 8m – 15m | 15m – 45m | Up to 50m (Building Height) |
| Primary Steel Grade | Q355B / Q460 Structural Carbon Steel | Q235B / Q355B High-Formability Cold Rolled | High-Tensile Cold-Formed Structural Steel |
| Crane Load Capacity | 1.0 Ton – 15.0 Tons (Bridge Crane) | 1.0 Ton – 3.5 Tons (Pallet Stacker) | Integrated Crane & Roof Truss Wind Load |
| Deflection Limits | L/500 Beam Horizontal Deflection | L/750 Column Vertical Rigidity | Compliance with Eurocode 3 / ANSI MH16.1 |
| Surface Protection | Heavy-Duty Electrostatic Powder Coat | Epoxy Powder / Continuous Galvanized | Hot-Dip Galvanized (HDG) / Ultra-Durable Powder |
Future Procurement Trends in Crane Racking Systems
How smart warehouse automation, modular OEM manufacturing, and carbon-neutral structural engineering are reshaping global supply chain investments.
1. Shift Toward Fully Rack-Supported Automated Buildings (RSB)
Enterprise buyers are transitioning away from conventional brick-and-mortar warehouse construction. Future procurement mandates favor Rack-Supported Buildings where the racking matrix directly supports wall cladding, roof structures, and overhead crane rails. This construction methodology reduces total real estate capital expenditure (CapEx) by 25% to 35% and accelerates commissioning timelines by up to 6 months.
2. Integration of Digital Twin & IoT Structural Sensors
Modern OEM crane supported racking contracts increasingly specify embedded strain gauges, laser deflection sensors, and vibration monitors along top runway beams. Connected via WMS/WCS API protocols, these IoT sensors provide real-time telemetry on frame stress, warning logistics managers of structural overload or crane track misalignment before catastrophic mechanical failure occurs.
3. High-Efficiency Cold Chain Storage Adaptation
With frozen food and pharmaceutical logistics surging globally, procurement teams are demanding crane-supported racking engineered for sub-zero operating environments (-30°C). OEM manufacturers must utilize specialized low-temperature impact-resistant steel alloys and zero-embrittlement powder coatings to resist thermal contraction stress while accommodating automated stacker crane thermal management.
4. Modular OEM Customization & Rapid Field Assembly
Global buyers now prioritize suppliers capable of delivering precision-punched, boltless or high-grade bolted frame connections that require no on-site welding. Prefabricated crane runway brackets, factory-welded saddle plates, and standardized export container packaging significantly cut local millwright labor costs in North America, Europe, and Australia.
Industrial Evolution & Global Manufacturing Standards
Navigating global structural codes, ESG compliance, and precision manufacturing capabilities required for enterprise procurement.
Why Partner with Rackzzszn Storage Equipment
Over two decades of structural manufacturing excellence, advanced automated production lines, and complete end-to-end export services.
In-House Engineering & Custom OEM/ODM Design
Our staff of over 300 experienced professionals includes dedicated structural engineers and R&D specialists who design custom 2D structural CAD elevation drawings, 3D BIM models, and FEA load calculation reports matched precisely to your warehouse ceiling height, building column grid, and crane load profiles.
South China's Longest Automatic Powder Coating Line
Equipped with over 80 advanced automated production machines—including high-precision roll-forming mills, automated robotic welding cells, multi-station CNC punching presses, and the longest continuous powder coating spray line in South China, capable of spraying three custom colors in a single automated pass for maximum corrosion resistance and finish uniformity.
Rigorous Full-Process Quality Assurance
SGS-verified and audited manufacturing processes. Every production batch undergoes strict raw material steel coil thickness checks, ultrasonic weld seam inspections, coating adhesion cross-hatch testing, and dynamic load-deflection test assembly prior to export container loading.
End-to-End Export & Site Support Services
From initial site survey measurements and technical consultation to export-optimized steel bundle packaging, customs documentation, installation manual assembly guides, and optional on-site engineering installation guidance, we provide turn-key peace of mind for overseas projects.
Ready to optimize your facility height with a custom crane supported racking system?
Get CatalogTechnical & Sourcing Procurement FAQ
Expert answers to standard structural engineering, customization options, and global shipping questions regarding crane supported pallet racking.
What is the main advantage of a Custom Crane Supported Pallet Racking System over freestanding crane gantries? +
How do your engineers calculate load capacities and structural deflection for crane integrated racks? +
Can crane-supported racking be installed in existing warehouse buildings? +
What customization options (OEM/ODM) are available for crane mounting brackets and rail profiles? +
What surface treatments do you recommend for heavy-duty crane racking and cold storage applications? +
How are overseas shipments packaged to prevent transit damage to heavy structural components? +
What documentation and installation guidance do you provide for international projects? +
Engineered Structural Storage Solutions tailored for your Facility
Contact our senior engineering team today for site investigation, 2D/3D layout design, FEA structural calculations, and direct OEM factory pricing.
Get Catalog