Featured Industrial Storage & Conveyor Hardware
Precision-engineered pallet racking units, automated shuttle systems, and heavy-duty load platforms designed for seamless integration with OEM automated conveyors.
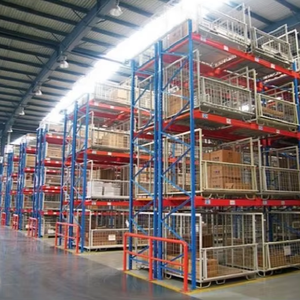
Heavy-Duty Steel Pallet Rack, Powder-Coated Finish, Adjustable Size, Customizable Load-bearing Panels & Colors
Get Catalog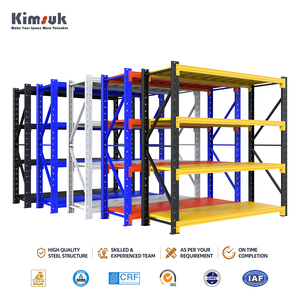
Boltless Adjustable Heavy Duty Load-Bearing 500kg/Layer Steel Racks Warehouse Industrial Stack Storage Racking Shelving System
Get Catalog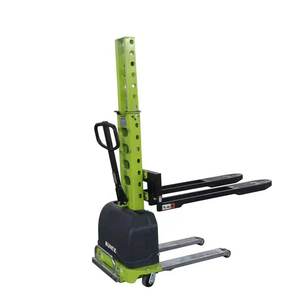
Runtx Brand Self Loading Electric Hand Pallet Stacker Self Loading with Car Lifting Stacker
Get Catalog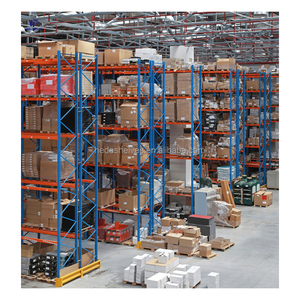
Discount Pallet Racking Industrial Pallet Shelving Units Steel Pallet Racks For Sale
Get Catalog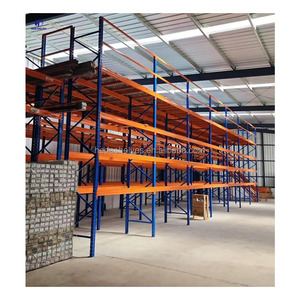
Warehouse Heavy Duty Steel Loft Platform Shelf Storage Attic Rack Pallet Racking Supported Mezzanine Floor Racks System
Get Catalog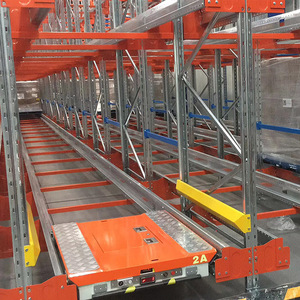
Jracking CE-Certified Radio Shuttle Rack System Space-Saving & Automated Storage Racking For Cold Storage Warehouses
Get Catalog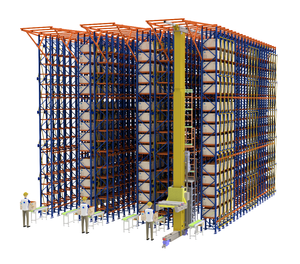
Labor Saving ASRS Customized Automatic Storage Retrieval Racking Systems
Get Catalog
Heavy Duty Storage Rack Pallet Rack System Shelf For Industrial Storage Rack
Get CatalogCustom OEM Pallet Conveyor Storage System Architecture & Metallurgical Rigor
A definitive technical guide for procurement directors, logistics engineers, and systems integrators seeking high-density automated material handling setups.
High-Tensile Structural Steel Specifications
Modern automated pallet conveyor storage systems require strict structural tolerances. Standard commercial steel often fails under repetitive dynamic loading cycles generated by high-speed pallet conveyors and automated guided vehicles (AGVs). We utilize cold-rolled Q235B and high-yield Q355B structural steel profiles featuring continuous column punching and specialized beam connector tabs.
This structural approach guarantees that vertical deflections remain strictly below L/200 under full static load capacity (up to 4,500 kg per level), preserving precise mechanical alignments between chain/roller conveyors and automated shuttle transfer mechanisms.
Seismic Engineering & Dynamic Impact Resistance
Integrating heavy powered roller conveyors directly onto pallet racking framing creates dynamic vibration vectors. OEM custom engineering must account for kinetic energy dissipation during emergency stops, directional switches, and pallet buffer accelerations.
Our OEM framing solutions incorporate cross-aisle bracing, floor-anchored footplates with chemical expansion bolts, and heavy-duty safety pins that resist unexpected vertical uplift forces caused by high-throughput conveyor sorting equipment.
| Storage & Conveyor System Type | Maximum Load Capacity | Throughput Efficiency | Automation Compatibility | Primary Industrial Application |
|---|---|---|---|---|
| Automated Driven Roller Conveyor Rack | 1,500 kg / pallet unit | Extreme (120+ pallets/hr) | Full WMS / WCS API Integration | E-commerce fulfillment & Fast-Moving Consumer Goods (FMCG) |
| Heavy-Duty Radio Shuttle Conveyor Grid | 2,000 kg / pallet unit | High (60–90 pallets/hr) | Semi-Automated PLC / Remote Control | Cold Storage (-30°C), Food & Beverage high-density buffer |
| ASRS Stacker Crane & Conveyor Interface | 3,000 kg / pallet unit | Ultra-High (Continuous 24/7) | Fully Automated Closed-Loop Control | Automotive manufacturing, chemical handling & heavy spares |
| Selective Pallet Conveyor Buffer Bay | 4,500 kg / shelf level | Moderate (30–50 pallets/hr) | Forklift + Infeed Conveyor Deck | Third-Party Logistics (3PL) & general inventory distribution |
Pallet Conveyor & Storage System Future Development Trends
Understanding shifting global supply chain dynamics: How OEM customized pallet conveyor storage systems are evolving toward energy efficiency, modular flexibility, and AI-driven control interfaces.
1. Smart IoT Sensor & WCS Native Integration
The traditional wall between static pallet racking and active conveyor hardware is disappearing. Modern OEM buyers require pre-drilled structural conduits, sensor brackets, and cable trays integrated directly into upright beams. Real-time vibration sensors and automated photoelectric switches track pallet movements, providing predictive maintenance alerts to prevent line stoppage.
2. Energy Recovery & Zero-Carbon Logistics
Energy cost reduction is now a primary KPI for distribution center managers. Next-generation gravity flow conveyors, regenerative motor rollers (24V DC brush-less motors), and light-weighted high-tensile alloy shuttle units consume up to 40% less electrical energy. Modern surface treatments prioritize zero-VOC electrostatic powder coatings baked at precise thermal cycles.
3. Modular OEM Plug-and-Play Standardization
Customization no longer implies long lead times. Leading OEM manufacturers maintain standardized sub-assembly modules (motorized roller sections, chain transfer turnables, upright frames) that plug into standardized boltless connectors. This enables fast layout scalability, allowing enterprise hubs to expand floor storage capacity rapidly.
Ready to Optimize Your Warehouse Layout & Storage Throughput?
Provide your building CAD drawings and load targets to receive a free 2D/3D engineering design layout and competitive direct-factory quotation within 24 hours.
Enterprise Strengths & OEM Manufacturing Authority
Rackzzszn Storage Equipment Co., Ltd. (Guangzhou Maobang) brings over two decades of heavy industrial manufacturing capability to global B2B clients.
20,000 m² In-House Production Facility
Equipped with over 80 advanced production machines including automated continuous roll-forming lines, precision CNC punching, robotic welding stations, and automatic edge-bonding equipment. We handle raw material coil slit-to-finish without subcontracting risks.
SGS Audited & CE Certified Quality Control
Strict ISO9001 internal quality audit processes. Every batch of steel coils undergoes tensile strength testing and coating thickness evaluation. Our products meet international racking standards including FEM 10.2.02 and RMI specs.
Longest Automatic Spray Line in South China
Our state-of-the-art continuous electrostatic powder coating tunnel allows up to three custom colors to be applied in a single pass. This ensures uniform film adhesion (60–80 microns), superior rust resistance, and accelerated order fulfillment.
300+ Skilled Staff & Engineering Specialists
With 200+ dedicated production technicians and 100+ specialized engineering, QC, design, and purchasing personnel, over 80% of our frontline workforce possesses 10+ years of structural steel fabrication expertise.
Proven Export Expertise to 60+ Countries
Over 1,000 containers shipped annually to North America, Europe, Southeast Asia, Australia, and the Middle East. Trusted by industry leaders including Toyota, Haier, Panasonic, SF Express, China Post, and JD.com.
End-to-End Lifecycle Services
From site survey, verified floor level measurements, and 2D/3D custom layout drawings to overseas installation guidance, structural inspection schedules, and original replacement spare parts delivery.
Frequently Asked Questions on Custom OEM Pallet Storage Systems
Direct answers from our senior logistics engineers regarding engineering parameters, site measurement risks, cold storage applications, and overseas assembly support.
Do you design custom racking & pallet conveyor layouts tailored to specific warehouse spaces?
Why is verified on-site dimensional measurement vital before finalizing custom racking orders?
Which specialized racking configuration best handles long, irregular, or heavy industrial goods?
Can your OEM pallet conveyor and racking systems operate reliably in sub-zero cold storage facilities?
What installation assistance do you provide for large-scale overseas logistics projects?
Partner with a Trusted OEM Storage System Manufacturer
Contact our engineering desk today to discuss product specifications, custom dimensions, OEM pallet conveyor integration, and project pricing.
Get Catalog