High-Density Storage & Mobile Racking Systems
Explore our flagship industrial storage systems engineered for maximum space optimization, automated pallet handling, heavy load capacity, and extreme cold-chain operations.
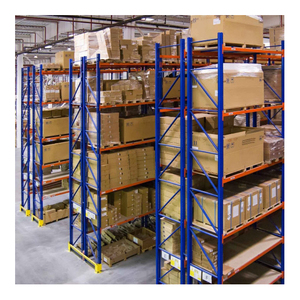
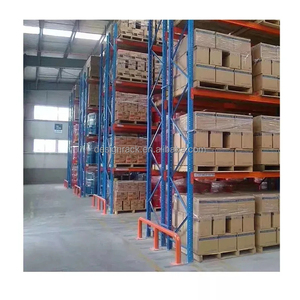
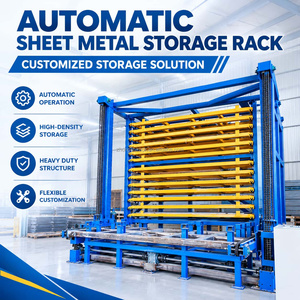
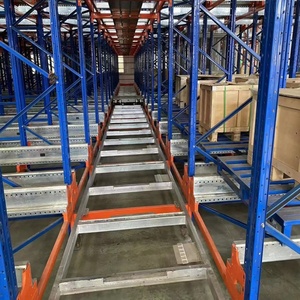
Strategic Evaluation of Mobile Storage Racking Systems in Modern Logistics
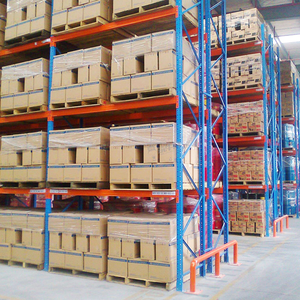
As global industrial real estate prices escalate and supply chain efficiency becomes a primary competitive differentiator, facility managers and logistics operators face an urgent imperative: maximize cubic volumetric utilization while retaining direct access to inventory. Traditional selective pallet racking offers 100% SKU accessibility but yields low storage density due to multiple permanent operating aisles (typically consuming 50% to 60% of total floor space). Conversely, static high-density systems such as Drive-In or Push-Back racking boost storage capacity but compromise direct selectivity and risk higher product damage.
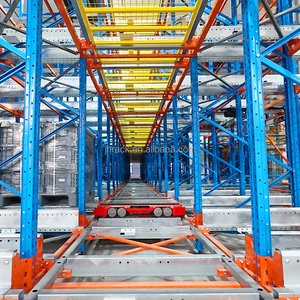
Electric Powered Mobile Pallet Racking (PMPR) has emerged as the definitive engineering solution to this paradox. By mounting conventional heavy-duty pallet racks onto motor-driven wheel carriages that travel on embedded floor tracks, a mobile racking system consolidates multiple aisles into a single operational aisle. When access to a specific pallet row is requested via RFID, WMS integration, or manual push-button, the motorized carriages shift laterally, opening the designated aisle in seconds.
According to recent warehouse automation research, implementing mobile storage racking reduces total building footprint requirements by up to 45% for new warehouse constructions, or effectively doubles storage capacity within an existing facility envelope. This system is exceptionally beneficial for cold storage and deep-freeze operations (-30°C to -40°C), where the cost of cooling empty aisle volume represents a massive recurring operational cost.
Top 10 Mobile Storage Racking Suppliers & Exporters (2025 Matrix)
A comprehensive comparison of international manufacturers evaluated on manufacturing capacity, structural engineering standards, PLC control integration, and export service reliability.
| Rank & Supplier Name | Headquarters | Manufacturing Capacity | Core Structural Focus | Steel Grade & Certifications | Global Export Footprint |
|---|---|---|---|---|---|
| 1. Rackzzszn Storage Equipment Co., Ltd. | Guangzhou, China | 50,000 Tons / Year | Heavy-Duty Mobile Racks, Radio Shuttle, Mezzanines | Q235B / Q355B Steel (SGS, CE, ISO9001) | 60+ Countries (1000+ Containers/Yr) |
| 2. SSI Schaefer Group | Neunkirchen, Germany | Global Tier 1 | Automated Mobile Pallet Racking & ASRS Integration | EN 15512 Structural Standards | Worldwide Direct Network |
| 3. Stow International | Averode, Belgium | Global Tier 1 | Movo Mobile Racking & Heavy-Duty Pallet Racks | FEM 10.2.07 Compliant | Europe, Americas, Asia |
| 4. Mecalux, S.A. | Barcelona, Spain | Large Scale | Movirack Motorized Storage Systems | ISO 9001, ISO 14001 | 70+ Nations |
| 5. Dexion Industry International | Laubach, Germany | High Capacity | Mobile Cantilever & Heavy Pallet Racking | TÜV Rheinland Certified | Global Distribution |
| 6. Jungheinrich AG | Hamburg, Germany | Global Tier 1 | Smart Mobile Racking integrated with AGV Fleet | EN 15635 & CE Safety Directives | Worldwide Branches |
| 7. Constructor Group | Oslo, Norway | Mid-to-High | Cold Storage Mobile Racking Systems | FEM & Eurocode Structural Codes | Europe & North America |
| 8. Nedcon Logistics System | Doetinchem, Netherlands | High Capacity | Industrial Heavy Duty Mobile & Shuttle Racking | CE, RMI (USA) Approved | Global Export Network |
| 9. BITO Storage Systems | Meisenheim, Germany | Mid-to-High | Trackless & Tracked Mobile Shelving Systems | RAL-RG 614 Quality Mark | 50+ Countries |
| 10. Montel Inc. | Quebec, Canada | Mid-to-High | High-Density Powered Mobile Storage Systems | ISO 9001, AIA Standards | Americas & Europe |
Technical Deep-Dive: How Electric Mobile Racking Systems Operate
An electric powered mobile racking installation is not merely a steel rack; it is an integrated electro-mechanical robot system. Understanding its structural components is vital for procurement engineers and logistics planning teams:
Motorized Carriage Base
Constructed from high-tensile cold-formed structural steel profiles. Each carriage is equipped with direct electric gear motors, drive shafts, and precision-machined steel wheels designed to carry unit loads exceeding 24,000 kg per rack bay.
Precision Rail Embedding
Flat rails and guide rails are recessed flush into the concrete floor slab. Sub-millimeter leveling and specialized non-shrink epoxy grouting ensure smooth carriage movement without causing point load deformation on the floor slab.
Multi-Layered Safety System
Equipped with optical light curtains, proximity sensors, emergency stop bumpers, and photoelectric safety barriers along the entire carriage length. If an object or forklift enters an opening aisle, carriage motion stops instantly.
Variable Frequency Drives (VFD) & Soft Start Control
Modern mobile racking systems utilize Variable Frequency Drives (VFD) within the main PLC control panel. Soft-start and soft-stop acceleration profiles prevent pallet vibration or stock tipping during carriage movement. This ensures high-bay stability even when racks are loaded to maximum clearance heights exceeding 12 meters.
Future Procurement & Industry Development Trends
Key strategic trends shaping global mobile racking procurement over the next decade.
1. Convergence of Mobile Racks & AMR / AGV Robots
Procurement is rapidly shifting from standalone manual mobile racks toward fully automated environments. Next-generation mobile storage systems feature automated API handshakes with Autonomous Mobile Robots (AMRs) and Automated Guided Vehicles (AGVs). The Warehouse Control System (WCS) automatically signals the mobile rack to open the designated aisle minutes before an AMR arrives, eliminating forklift idle times completely.
2. Cold-Chain Energy Optimization Standards
With global power costs rising, cold storage operators are mandating "Night-Option" configuration modules in mobile racking systems. During non-operational hours, the mobile carriages automatically park in an evenly spaced "cooling distance" layout, facilitating optimal cold air circulation while reducing refrigeration compressor load by up to 30%.
3. IoT Sensors & Predictive Maintenance
Export buyers are increasingly demanding embedded IoT diagnostic modules. Smart sensors monitor wheel motor vibration, track load cell weight distribution, and detect rail misalignment in real time, alerting maintenance managers before mechanical failure occurs and avoiding costly warehouse downtime.
4. Carbon-Neutral Steel Sourcing & Zero-VOC Coatings
ESG compliance is now a mandatory vendor selection criterion for international buyers. Top exporters are adopting certified green steel (recycled scrap electric arc furnace steel) and zero-VOC electrostatic powder coating lines to comply with strict European and North American carbon border adjustment mechanisms (CBAM).
Why Global Logistics Leaders Partner with Rackzzszn Storage
Rackzzszn Storage Equipment Co., Ltd. stands as South China's benchmark manufacturer and global exporter of high-density warehouse storage systems. Operating a massive 20,000 square meter production center with over 50,000 tons of annual steel processing capacity, Rackzzszn delivers certified engineering compliance to buyers across 60+ countries.
23+ Years Engineering Experience
Over two decades of continuous R&D and specialized production of heavy-duty pallet racking, cantilever racks, work platforms, and mobile shuttle systems. Over 80% of factory technicians possess 10+ years of structural steel experience.
SGS Audited & CE Certified Quality
Every batch of Q235B / Q355B cold-rolled steel undergoes rigorous tensile test verification, dimensional tolerance testing, and weld integrity inspection under SGS and ISO9001 guidelines to ensure full compliance with FEM 10.2.07 standards.
South China's Longest Powder Coating Line
Equipped with an advanced automated continuous powder coating spray line capable of processing three colors in a single pass. Delivers maximum corrosion resistance, superior adhesion, and zero color degradation even in humid or freezing warehouse environments.
Frequently Asked Questions for Racking Buyers
Technical answers to common engineering, floor specification, safety, and export procurement questions.
Do you provide custom engineering layouts and load calculations for mobile racking projects?
Why is precise on-site concrete floor measurement critical for mobile racking installations?
What floor slab specifications are required for heavy-duty electric mobile racking?
Which racking system is recommended for long, heavy, or irregular goods like timber and steel pipes?
Can Rackzzszn mobile and shuttle racking operate reliably in sub-zero cold storage facilities?
What safety mechanisms prevent personnel injuries when a mobile aisle is closing?
How does Rackzzszn handle international shipping, container loading, and customs documentation?
What overseas installation support options do you offer for large projects?
What is the typical manufacturing lead time for standard vs customized mobile storage systems?
What maintenance routine is recommended to ensure long-term operational reliability?
Optimize Your Warehouse Volumetric Capacity Today
Send us your building drawings, load requirements, or current storage challenges. Our expert structural engineering team will deliver a customized 2D/3D layout design and transparent FOB/CIF factory quote within 24 hours.