Engineering-Grade Racking Systems
Custom OEM/ODM structural pallet racks designed for seamless integration with stacker cranes, overhead cranes, and automated material handling equipment in UK facilities.
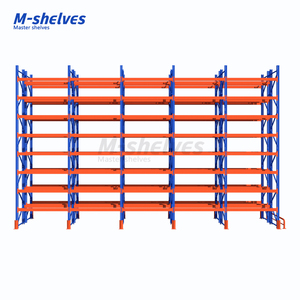
Shelf Heavy Duty Adjustable Corrosion Protected Customizable Size Pallet Beam Racking for Large Logistics Distribution Warehouse
Contact Us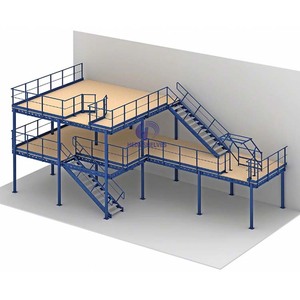
High Q235 Steel Warehouse Multi-level Mezzanine Flooring Rack Industrial Storage Platforms Shelving
Contact Us
Jracking Modular Design Warehouse Storage Shelf CE Certified Heavy Duty Pallet Racking System for Cold Room
Contact Us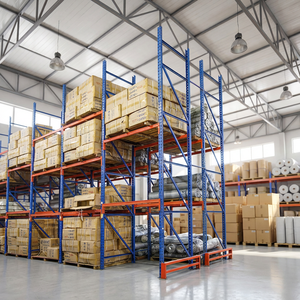
Galvanized Steel Pharma Industrial Warehouse Heavy Duty Pallet Rack
Contact Us
VNA Pallet Racking System Narrow Aisle High Bay Storage Solutions
Contact Us
Durable 5-Layer Heavy Duty Cold Rolled Steel Powder Coated Shuttle Warehouse Racking High Density Automated Storage Racks Bulk
Contact Us
Heavy-Duty Steel Warehouse Rack Storage Double-Deep Pallet Multi-Level for Stacking and Storing in the Warehouse
Contact Us
Dongguan Manufacturer Factory 500kg Loading Capacity Medium Duty Warehouse Rack for Sale
Contact Us1. Technical Deep-Dive: Crane-Supported Pallet Racking Mechanics for High-Bay Automation
Crane-supported pallet racking—often deployed within Automated Storage and Retrieval Systems (AS/RS)—represents the absolute apex of structural warehouse engineering. Unlike conventional freestanding pallet racks, crane-guided high-bay systems perform dual structural roles: they support heavy unit pallet loads (ranging from 1,000 kg to over 3,000 kg per position) while simultaneously acting as the physical structural dynamic guide for top-running or bottom-supported stacker cranes (SRMs) and overhead hoist bridges.
When engineering crane-supported racking for the United Kingdom industrial landscape, structural tolerances must adhere to exceptionally stringent deflections. Under FEM 10.2.02 (Design of Automated Tall Rack Warehouses) and BS EN 15512:2020 (Steel Static Storage Systems), horizontal deflection under dynamic crane acceleration must not exceed H/1000 to prevent structural sway from inducing operational jams or triggering automatic E-stop sensors on laser-guided cranes.
Key Mechanical Interface Specifications:
- High-Yield Cold-Rolled Structural Steel: Engineered using premium Q355B and Q235B micro-alloyed steel profiles, providing high tensile strength and impact resistance under rapid crane acceleration.
- Integrated Crane Rail Beams: Top guide rails and crane runways are bolted or seamlessly welded directly into structural upright towers, utilizing machined fishplates to guarantee continuous rail alignment within ±1.5mm across 100-meter aisle runs.
- Deflection Control Mechanisms: Custom diagonal bracing matrix designed using Finite Element Analysis (FEA) to counteract dynamic braking forces generated by modern 240m/min stacker cranes.
- Custom Footplate Anchoring: Extra-thick structural shim plates with heavy-duty chemical anchors designed to transmit concentrated axial down-loads to UK concrete slab specifications (BS 8204 / TR34 Category 1 flatness).
2. UK Localized Application Scenarios & Strategic Regional Integration
The UK logistics market features a unique combination of high real estate acquisition costs, strict planning permissions for greenfield developments, and an aging stock of commercial buildings requiring retrofitting. OEM/ODM crane-supported racking provides an optimal engineering solution by maximizing vertical cubic meter usage without expanding building footprints.
Golden Triangle Logistics (M1/M6)
Ideal for automated distribution hubs in Daventry, Northampton, and Rugby requiring 18m to 30m high-bay automated pallet retrieval with zero floor-space waste.
Cold Storage & Deep Freeze Facilities
Deployed in UK cold chain networks (down to -30°C) across Grimsby and Immingham. High-density crane racking minimizes refrigerated volume, driving down energy bills.
Automotive & Aerospace Manufacturing
Serving automotive plants around the West Midlands and Sunderland. Supports heavy die storage, engine block pallets, and steel coil handling via integrated top hoists.
3. Structural System Selection Matrix for UK Procurement Officers
Selecting the correct racking architecture is critical to balancing initial capital expenditure (CapEx) against long-term operational efficiency (OpEx). The table below outlines key structural parameters comparing OEM/ODM crane-supported racking to conventional UK storage systems.
| System Architecture | Max Storage Height | Aisle Width Required | Crane / Equipment Interface | Floor Space Utilization | Compliance Standards |
|---|---|---|---|---|---|
| Crane-Supported High-Bay (AS/RS) | Up to 45 Meters | 1.4m – 1.6m | Stacker Crane / Top Rail Guide | 90% – 95% (Cubic Height) | BS EN 15512 / FEM 10.2.02 |
| Very Narrow Aisle (VNA) Racking | Up to 18 Meters | 1.6m – 1.9m | VNA Turret Truck / Wire Guidance | 75% – 80% | SEMA Code / BS EN 15635 |
| Automated Radio Shuttle Racking | Up to 12 Meters | Drive-In Style Lanes | Autonomous Shuttle + Forklift | 80% – 85% | BS EN 15095 / CE Marked |
| Standard Selective Pallet Rack | Up to 12 Meters | 3.0m – 3.5m | Standard Counterbalance / Reach | 40% – 50% | SEMA Guidelines |
4. Strategic Storage Trends Shaping the UK Warehousing Sector
As UK supply chains adapt to post-Brexit customs procedures, rising labor overheads, and stringent net-zero carbon targets, UK logistics managers are overhauling legacy storage infrastructure. Key trends driving the specification of custom OEM/ODM crane-supported systems include:
- Brownfield Site Maximization: With planning constraints restricting urban sprawl in green-belt areas around London and Manchester, companies are converting existing low-efficiency facilities into vertical high-bay automated sites.
- ESG & Decarbonization in Manufacturing: Procurement teams actively audit steel supply chains. Our factory utilizes high-efficiency automated powder-coating recovery systems and zero-waste recycling protocols, ensuring low embodied carbon footprint in exported structural steelwork.
- Integration of AI and WCS (Warehouse Control Systems): Crane-supported racks are increasingly fitted with embedded IoT sensors for real-time vibration tracking, structural stress analysis, and predictive maintenance.
5. Enterprise Manufacturing Excellence & OEM/ODM Capabilities
As an audited manufacturer with over 23 years of specialized experience in storage equipment fabrication, Rackzzszn operates a state-of-the-art 20,000 m² manufacturing plant capable of processing over 50,000 tons of structural steel annually. We provide full end-to-end OEM and ODM services for global integrators, general contractors, and rack distributors.
In-House Roll Forming & Punching
Over 80 automated roll-forming machines produce upright profiles with precise pitch accuracy, ensuring zero binding along crane guide rails.
South China's Longest Powder Coating Line
Equipped with an advanced continuous powder-coating spray line capable of processing up to three colors in a single automated pass for extreme corrosion resistance.
Robotic Precision Welding
Robotic welding arms execute consistent structural welds on beam connectors and crane attachment brackets, audited via non-destructive testing (NDT).
Complete OEM/ODM Workflow:
Our engineering office collaborates directly with UK client teams: from initial CAD site plan analysis and 3D FEA stress simulations to prototyping, trial assembly in factory, export packing in sea-worthy bundles, and comprehensive installation guidance.
6. Frequently Asked Questions (FAQ) for UK Procurement & Project Engineers
Do your racking systems comply with UK Building Regulations and SEMA standards?
Yes. All structural racking solutions serving the UK market are engineered in strict accordance with BS EN 15512 (structural design rules), SEMA Codes of Practice, and relevant UK Structural Building Regulations (Part A Structural Safety).
Can you custom-manufacture racking to interface with third-party stacker cranes?
As a specialized OEM/ODM manufacturer, we work directly with drawings provided by crane manufacturers (e.g., Dematic, Swisslog, Daifuku, SSI Schaefer) to ensure exact top-rail mounting geometries, guide tolerances, and electrical conductor bracket positions.
What anti-corrosion finishes are recommended for UK unheated warehouses or cold storage?
For standard ambient warehouses, our epoxy-polyester powder coating delivers superior scratch resistance. For high-humidity UK coastal environments or deep-freeze cold stores (-30°C), we supply hot-dip galvanized steel (EN ISO 1461 compliant) for permanent rust protection.
What is the typical lead time for export shipping to major UK container ports?
Production cycles generally range between 20 to 30 days depending on order tonnage. Ocean shipping to UK ports (Felixstowe, Southampton, London Gateway) typically takes 28 to 35 days. Freight-optimized container packing ensures maximum cubic loading efficiency.
Do you offer on-site measurement verification and installation guidance?
Yes. We provide complete structural assembly drawings, step-by-step installation manuals, and 3D video documentation. For major UK projects, on-site installation supervisors can be deployed to assist your local installation crews.
How do you handle structural steel quality assurance and raw material traceability?
Every batch of steel coil undergoes raw material tension and yield testing upon arrival. Mill Test Certificates (MTCs) confirming compliance with Q235B / Q355B (equivalent to S235 / S355 European grades) are issued with every export shipment.
Ready to Engineer Your UK High-Bay Crane Racking Project?
Connect directly with our senior structural engineering team for complimentary 2D/3D layout design, FEA structural reports, and transparent OEM factory-direct quotation.
Contact Us